PVLinkTech follows a waterproof connector quality control process that includes specification review, inspection checks, final verification, and clear documentation support before dispatch.
| Question | One-line answer |
|---|---|
| What waterproof connector quality control covers | Four gates: incoming components, in-process assembly, electrical and sealing tests, and a pre-shipment final inspection. |
| Which standard decides the IP rating | IEC 60529. It fixes IP67 at 1 m of water for 30 minutes and leaves the IP68 depth and duration to the manufacturer, so the condition is quoted with the rating. |
| What is the IP68 test condition | The condition is taken from the test record for that model rather than from a single company-wide figure, because IEC 60529 leaves the depth and the duration of IP68 to the manufacturer. Open the datasheet for the model on your order and the figure is there. |
| Can I get a pre-shipment inspection report | Yes, on request. It is written against the approved model, quantity, ratings and packaging for that order. |
| Do you allow third-party inspection | Buyers and their inspection agencies are welcome on a scheduled visit, and a video audit covers travel that is not practical. |
| How quickly does a standard order ship after inspection | Standard stock items are prepared for dispatch in 3 to 5 business days once the requirements and payment terms are confirmed. |
A batch that measures correctly at the end can still arrive wrong, which is why four gates sit between the order and the pallet instead of one. They run in sequence, because each one answers a different question about the same build.
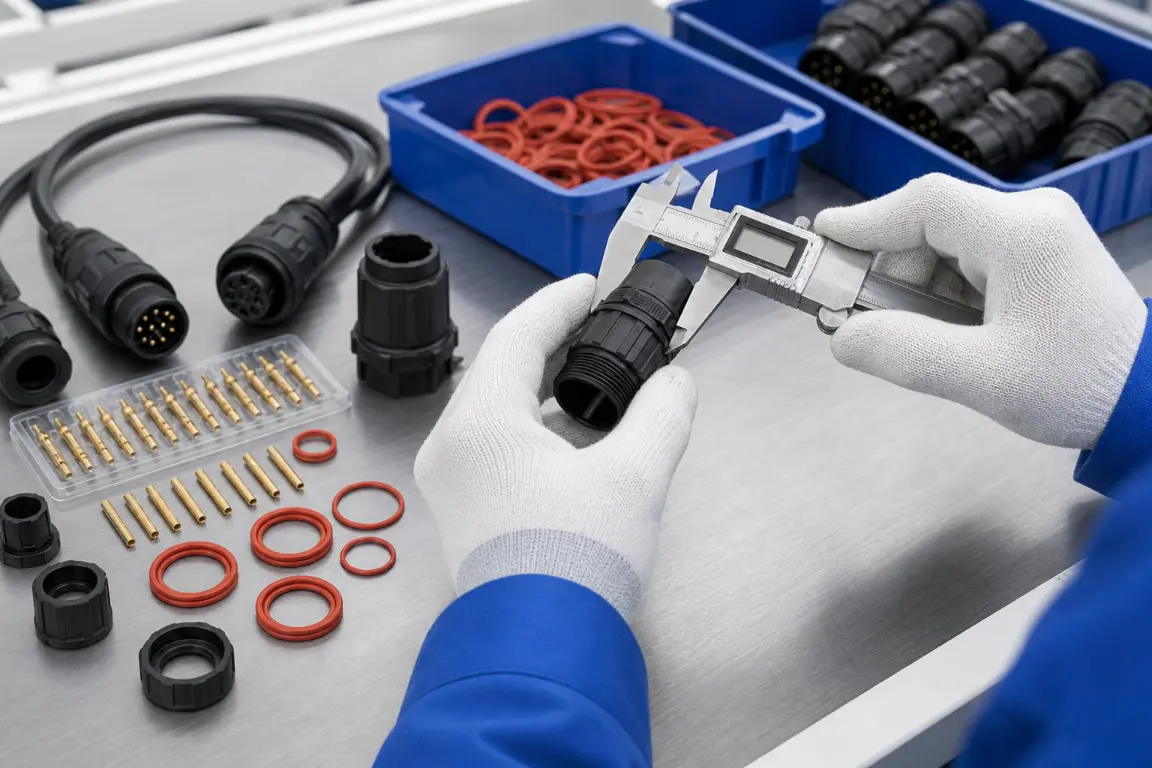
Inspection starts at the receiving bay, before anything is assembled. Housings, terminals, seals, cable and plating arrive from several suppliers, and each is checked against the drawing or the product requirement it was bought to: contact material and plating, seal dimensions, cable outer diameter and jacket material, and the molding details that decide whether the two halves will mate.
A housing or terminal that misses its requirement is stopped before it reaches assembly. That is the cheapest place to stop a problem in waterproof connector quality control, and the only one where a correction costs a message instead of a production slot.
Crimp height and pull-out force are checked on the terminals, and sealing parts are confirmed seated before the housing closes. The locking mechanism is worked by hand to confirm that it latches and releases. Polarity, wire sequence and pin position are read against the drawing for the model in the fixture, because a 3-pin connector wired as a mirror image passes every electrical test and fails at the installation.
Appearance is checked at the same station: flash, sink marks, color and print quality. The connector inspection process at this gate is a sequence of measurements rather than a final glance, and waterproof connector quality control puts a number on each one.
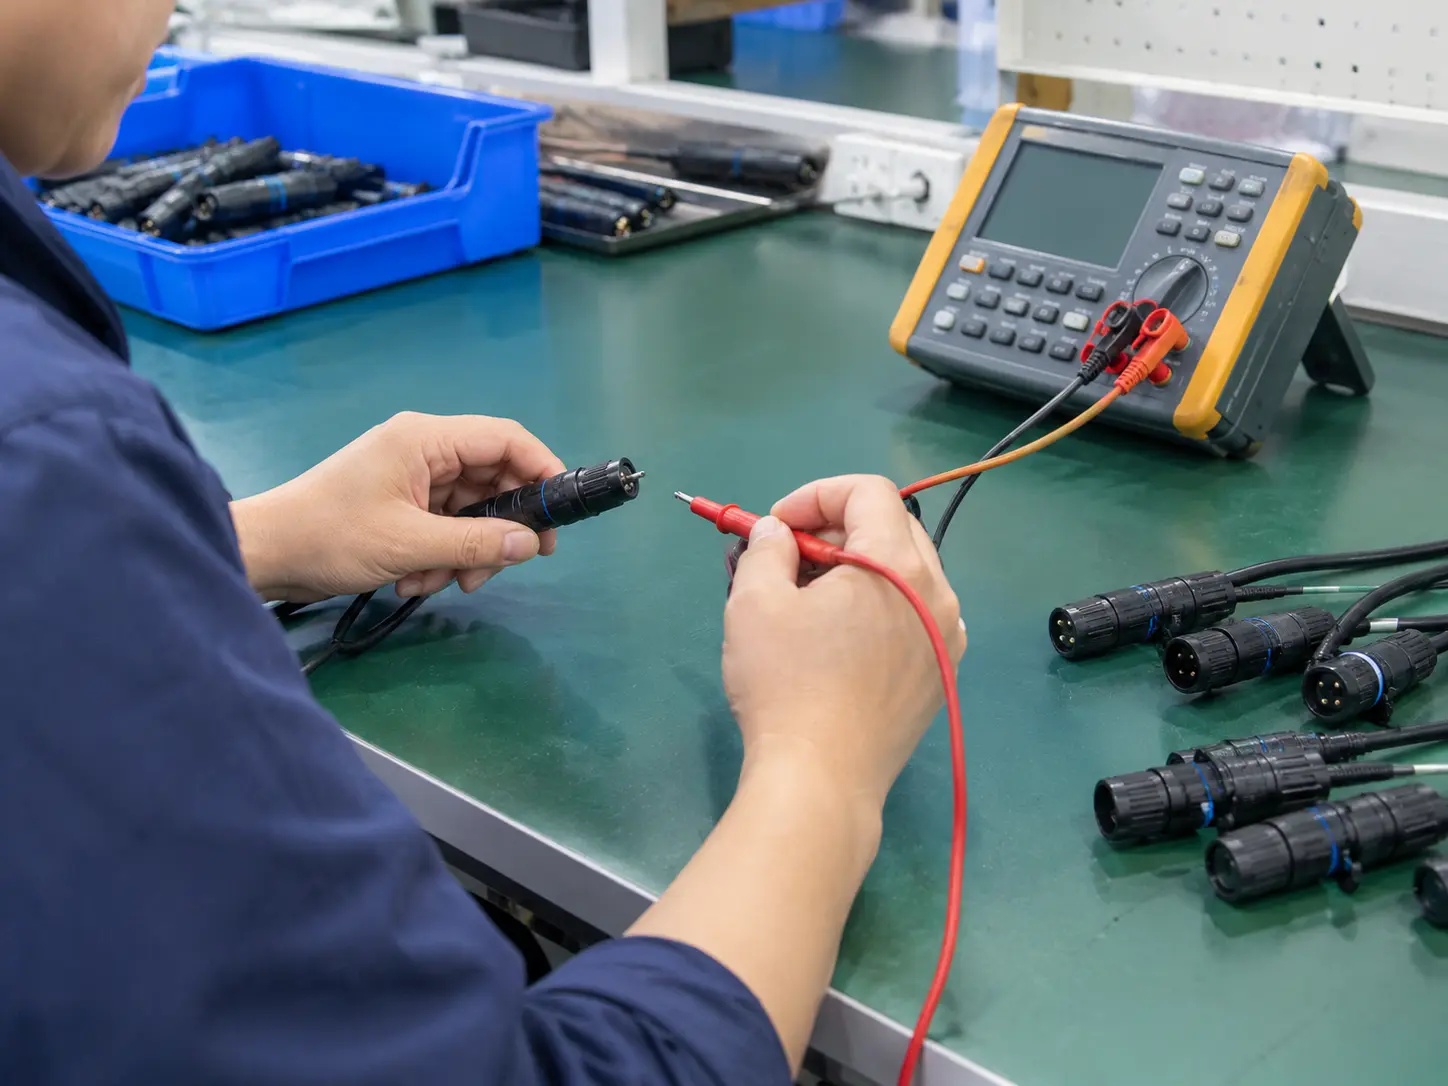
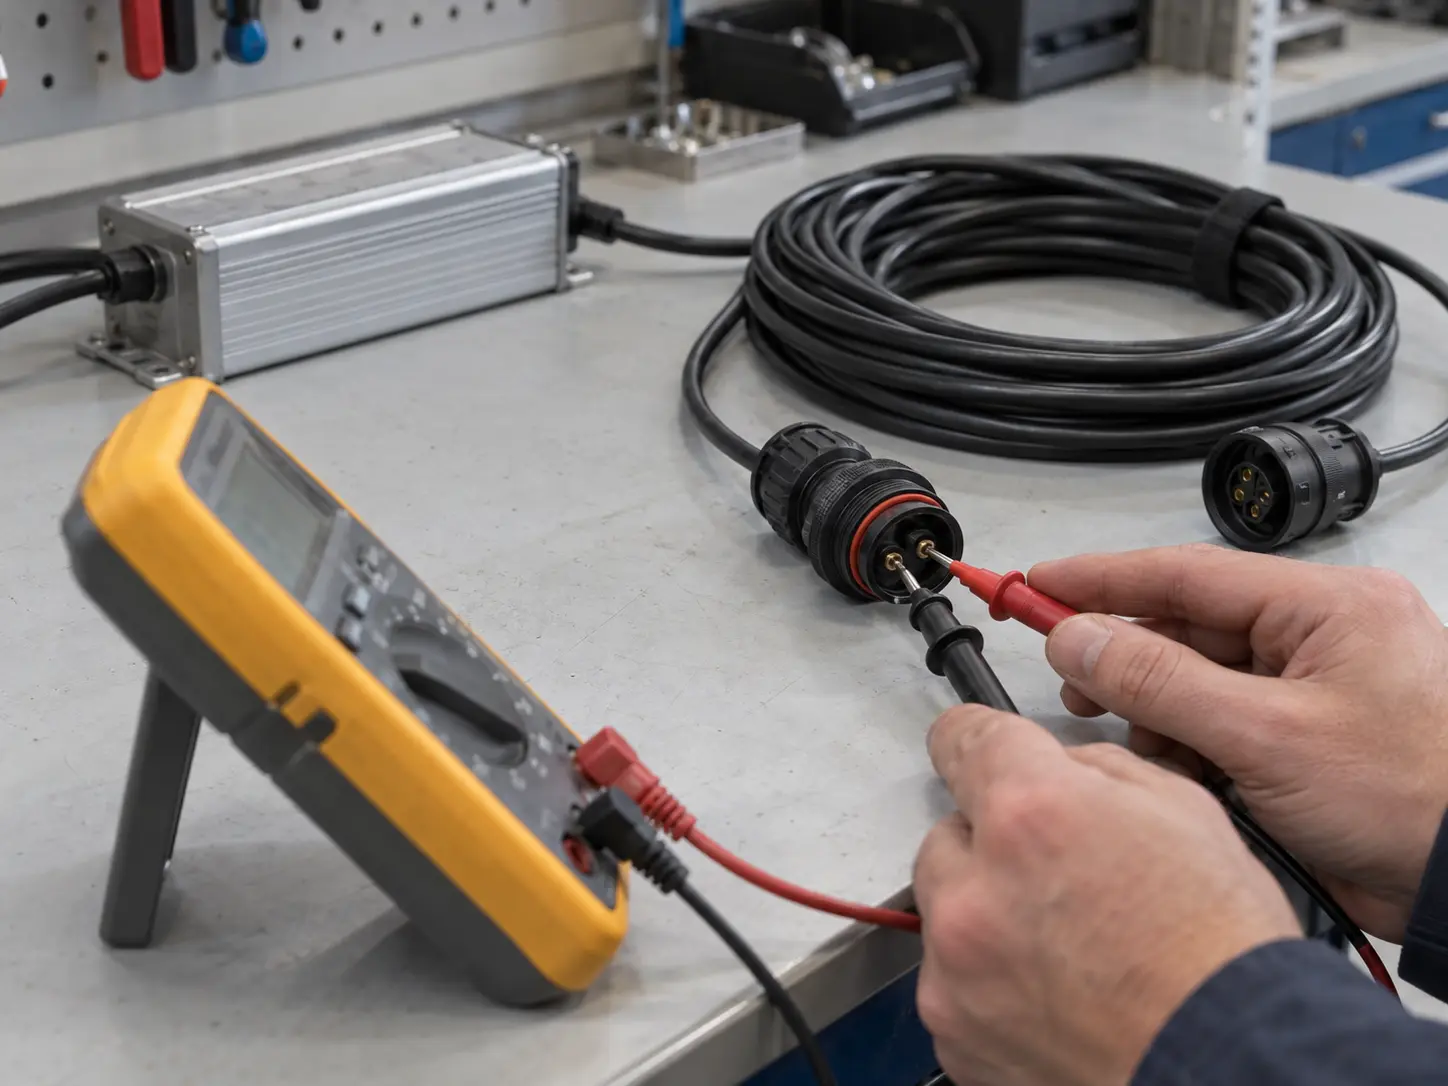
Dielectric withstand is applied at the voltage the applicable standard defines for the series. The contact resistance test is run in milliohms against the limit on the datasheet for that model, because a joint reading a few milliohms high is a hot spot with a delay on it.
Sealing is the part of waterproof connector quality control that leaves the bench and goes into a water tank. The IP68 waterproof test runs in an immersion tank at the condition recorded for that model, because IEC 60529 leaves the depth and the duration to the manufacturer. That record travels with the M686 junction box range datasheet, and with every panel and cable series we ship.
Salt spray covers the plated parts and the housing finish. Insertion and withdrawal force is measured on the mating pair to confirm the lock holds without force that would damage the seal. A test we do not run in-house goes to a third-party laboratory instead.
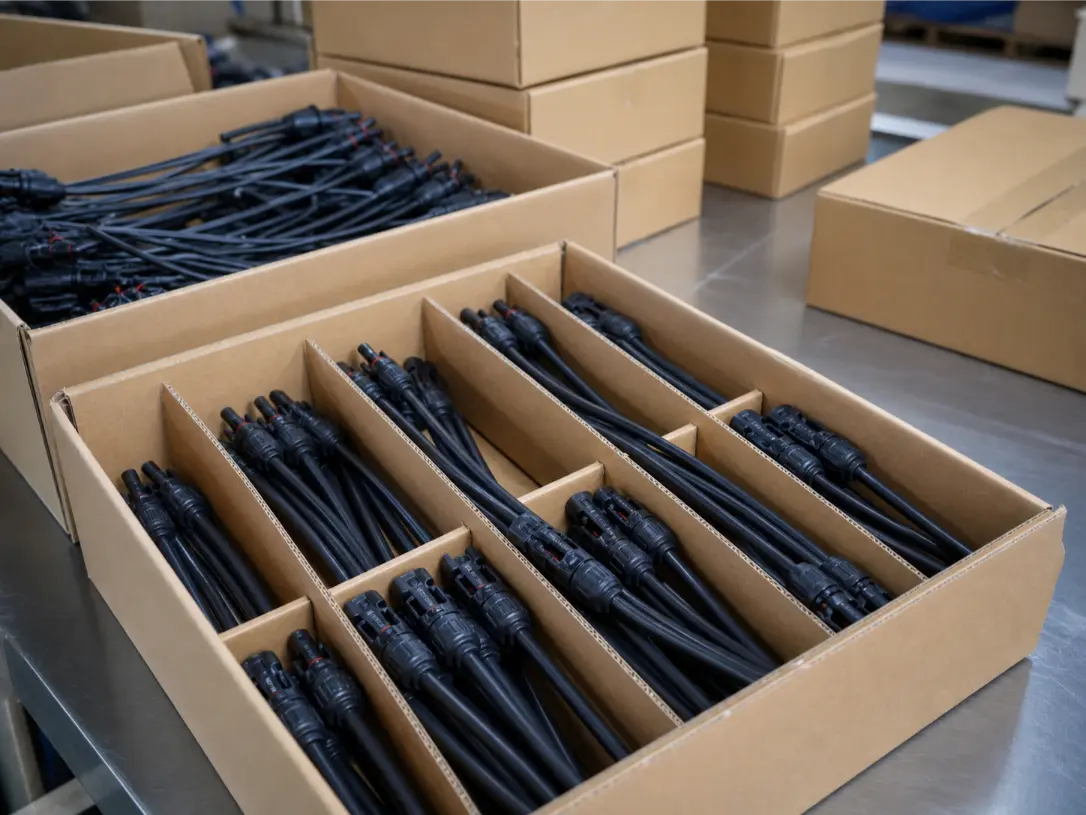
Every order gets a last look before packing: model, pin configuration, quantity, appearance, labels and packaging checked against what was ordered. A carton label naming the wrong model costs a buyer a receiving error, and the check itself costs minutes.
Custom printing, private labels and split packaging are confirmed here as well. Private label orders are separated from stock at this final stage of waterproof connector quality control, so artwork is better sent with the inquiry than after the goods are built.
Quality control is a sequence of measurements on a connector order, and a checkpoint earns its place only when a buyer can see where it sits in that sequence. Eight of them carry most of the weight, and each one is tied to a gate rather than to a person.
| What is checked | Gate | Why it matters to your project |
|---|---|---|
| Model and pin configuration | Gate 1 and Gate 4 | Prevents an incompatible mating pair and a wrong-model shipment. |
| Housing, terminal and plating materials | Gate 1 | Contact material and plating decide how the joint behaves after a few hundred mating cycles. |
| Seal dimensions and cable outer diameter | Gate 1 and Gate 3 | A seal matched to the wrong cable diameter is where water enters, not at the housing. |
| Crimp and wire termination | Gate 2 and Gate 3 | The crimp is one of the two interfaces that generates heat once resistance creeps up. |
| Locking mechanism, polarity and pin position | Gate 2 and Gate 4 | A latch that does not hold lets the halves part under vibration, and reversed polarity fails at commissioning. |
| Dielectric withstand and contact resistance | Gate 3 | Insulation and resistance are measured before dispatch instead of after a fault. |
| Immersion at the quoted condition | Gate 3 | Confirms the seal at the housing, the cable entry and the mating interface. |
| Labels, packaging and quantity | Gate 4 | A receiving error costs a stock correction and a second shipment. |
The list confirms the sequence. It does not replace the approved specification, and an order carrying a requirement outside it gets that requirement written into the order file, checked where it applies.
Waterproof connector quality control is decided before the first measurement, because every check here is written against a document rather than a habit. Four standards sit behind most of what runs on the line, and each one answers a different question.
IEC 60529 is the IP code standard, and it defines the degrees of protection an enclosure provides, including the immersion tests behind IP67 and IP68. IEC 62852 is the standard for DC connectors in photovoltaic systems, up to 1500 V DC and 125 A per contact, so a 1500 V DC architecture points at the energy storage connectors rather than at a 1000 V family. UL 1977 evaluates a connector as a component. UL 4128 is an Outline of Investigation for intercell and intertier connectors inside a battery system, covering up to 3000 V DC and permitting no connection or disconnection under load. That difference decides which document a cabinet reviewer wants, and it is set out in our note on reading BESS connector certificates .
The ISO 9001, IATF 16949, ISO 13485 and ISO 14001 certificates are system audits. They sit outside waterproof connector quality control, not inside it, and they cover how a plant plans work, controls changes, keeps records and manages environmental impact. None of them is evidence that a connector passed an electrical test. Where a customer specification is stricter than any document in the table, waterproof connector quality control follows the customer document, and the order file records it.
| Standard | Issued by | What it covers |
|---|---|---|
| IEC 60529 | International Electrotechnical Commission | Degrees of protection provided by enclosures, including the immersion tests behind IP67 and IP68. |
| IEC 62852 | International Electrotechnical Commission | DC connectors for photovoltaic systems, up to 1500 V DC and 125 A per contact. |
| UL 1977 | UL Solutions | Component connectors for data, signal, control and power applications. |
| UL 4128 | UL Solutions | Outline of Investigation for intercell and intertier connectors in battery systems, up to 3000 V DC, with no connection under load. |
| ENEC and the CB scheme | ENEC Agreement and IECEE | Third-party certification of lighting and electrical products, and the international test reports used as the basis for national approvals. |
| RoHS and REACH | European Union | Restricted substances in electrical equipment, and chemicals in articles. |
| ISO 9001, IATF 16949, ISO 13485, ISO 14001 | ISO and IATF | Management systems for general manufacturing, automotive, medical devices and environmental management. System audits, not product tests. |
The bench side of waterproof connector quality control is repeatable only when the machine behind the number is known; a supplier audit usually asks that question first.
| Test | What it verifies | Where it runs |
|---|---|---|
| Dielectric withstand | Insulation between live parts and the housing at the applicable standard voltage | In-house, on the production lot |
| Contact resistance | The crimp and the mated contact pair, measured in milliohms | In-house, on samples from each lot |
| Immersion | The seal at the housing, cable entry and mating interface | In-house immersion tank, at the quoted condition |
| Salt spray | Plating and housing finish under a salt-laden atmosphere | In-house cabinet, or a third-party laboratory when a project names one |
| Insertion and withdrawal force | The locking mechanism and the seal under normal mating | In-house, on the mating pair |
Buyers and their third-party inspection agencies are welcome at the plant, and a video call can walk your engineer through the stations when travel is not practical. Naming the equipment shortens an audit, because the machines behind waterproof connector quality control are read before the documents.
The paperwork is the part of waterproof connector quality control that a buyer still has months later. Every order leaves with a packing list that matches the carton labels and the confirmed model list.
Drawings and the datasheet for the ordered model come before dispatch. Published datasheets sit on the downloads page with no form in front of them. A pre-shipment inspection report is available on request, and it records the model, quantity, ratings and packaging approved for that shipment. It is the written trace of waterproof connector quality control for that order, not a general statement of good practice.
Where a model carries certification, the copy and its file number come from the certificates and compliance documents held for that model. A third-party certificate belongs to the manufacturer of the construction that was evaluated, so it cannot be reissued in a buyer’s name; what we confirm is that the part on your order is that construction.
Every shipment carries a 12-month warranty against manufacturing defects, alongside the waterproof connector quality control record for that order. A claim starts with photos or the returned sample, and the reply comes within 24 hours with a route forward: replacement, rework or technical guidance.
The first decision on a connector order is better made on a part you can hold than on a drawing, which is why a 1-piece evaluation order exists. Approve it against criteria written down before the parcel was opened, and connector sample testing sets out what to measure and where each limit should come from. Most waterproof connector quality control disputes trace back to a sample nobody measured against a written limit, and the bulk order inherits the argument.
Once the model and the requirements are confirmed, the agreed specification, labeling and packaging carry into repeat orders, and the same waterproof connector quality control runs against the same file.
A failed batch does not move until you know what failed and how many units are affected. A defect in a component or an assembly step is reworked, or the affected units are replaced. A failure that traces back to a requirement that never fit the application, such as a cable outer diameter that changes how the seal seats, belongs in the specification rather than in the batch.
Either way, what comes back to you is the measurement, the document it was compared against, and the count of units affected. Strip those three details out and waterproof connector quality control becomes a black box to the buyer.
Every order passes a final inspection before packing, and the electrical, sealing and mechanical checks run at the gates before it. On a standard order, waterproof connector quality control follows the same four gates. What is inspected inside them depends on the model and the approved requirement, so the sequence is confirmed with the quotation rather than assumed from a photo.
The IP68 condition quoted in waterproof connector quality control is the one recorded for that model, not a single company-wide figure, because IEC 60529 leaves the depth and the duration to the manufacturer. The figure your project is reviewed against is on the datasheet and repeated in the pre-shipment file, so it can be traced to a document.
Yes. Ask with the order, and it is written against the approved model, quantity, ratings and packaging for that shipment, which is what waterproof connector quality control recorded at the last gate before dispatch. If your incoming inspection has a checklist, send it early and the report matches the points you measure.
A scheduled visit is welcome, and a video audit covers projects where travel is not practical. Book it inside a production run so the checks can be watched as they happen.
Both routes come with the same record: what was measured, the document it was compared against, and how many units were affected. A component or assembly defect is reworked, or the affected units are replaced. If the failure traces back to a requirement that never fit the application, the change goes into the specification, and the revision is confirmed with you before the batch moves. A failure reported this way is waterproof connector quality control working as intended.
For project and custom orders, yes. Send the artwork, the packaging requirement and the quantity in advance; the detail is confirmed at the sample stage, and the pre-shipment gate checks that the artwork you approved is the artwork that arrives.
A 1-piece evaluation order is available where the model is in production. Send the application, the model and the cable you will use, and the sample route is confirmed with the quotation. Approving the sample against written criteria is what makes the bulk order repeatable.
Standard stock items are prepared for dispatch in 3 to 5 business days once the requirements and payment terms are confirmed. Custom builds, samples and special packaging take longer, and the lead time is confirmed in writing.
Send the model, the application and the ratings your project is reviewed against, so waterproof connector quality control is planned against your numbers. What comes back is the set of checks that apply to that order, the documents held for the model, and a sample route before the bulk order.
LET’S BUILD YOUR CONNECTION SOLUTION
Share your application, specifications, and estimated quantity. Our team will recommend a suitable connector solution and provide a quotation.
Low MOQ · OEM & ODM · Product Selection Support · Fast Quote Response