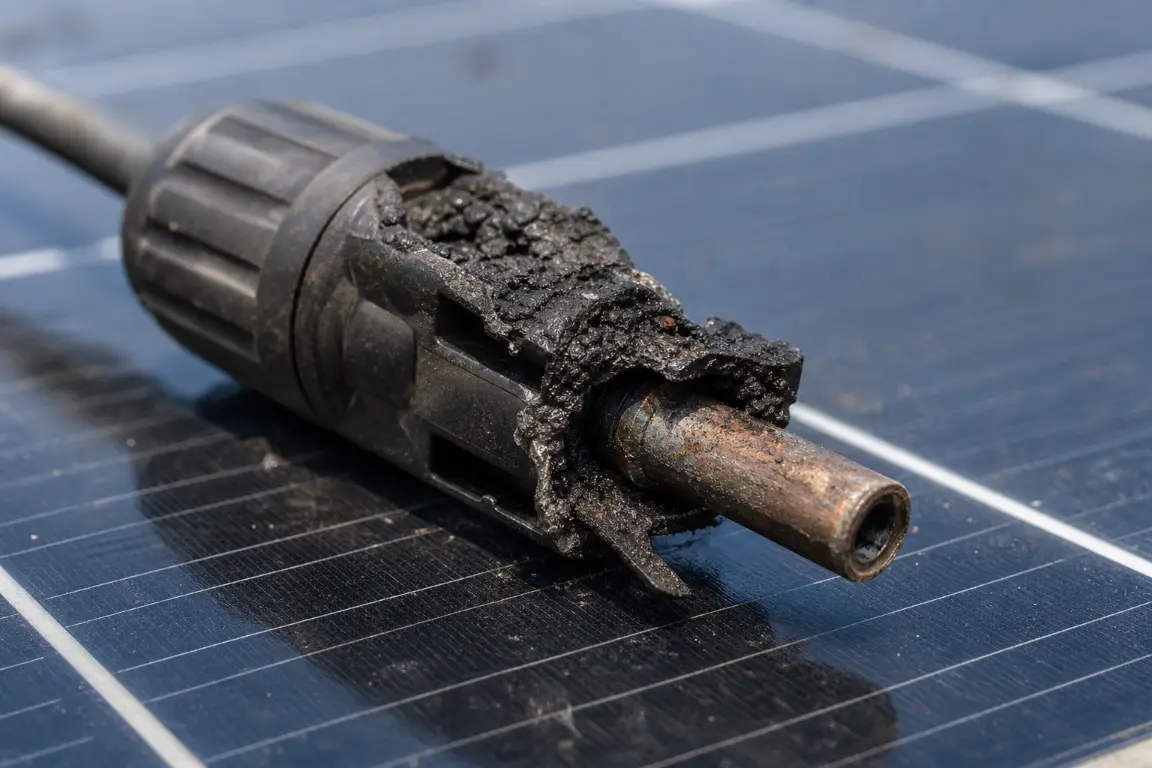
Most solar connector overheating starts at one of two interfaces: the cable-to-terminal crimp, or the mated contact pair. When resistance at either interface rises, the joint turns current into heat. The housing is usually the last part to fail, and melting is the last stage of a failure that has been building for months.
Quick answer
Solar connectors overheat or melt when electrical contact resistance rises at two critical interfaces: the wire-to-terminal crimp or the mated pin-and-sleeve contact pair. While a healthy MC4-style PV connector maintains contact resistance below 0.5 mΩ (per IEC 62852:2014+A1:2020), field failures—most commonly improper field crimping, cross-mating different connector brands (violating NEC 690.33(C)), incomplete locking, or moisture ingress—can push resistance into tens of milliohms. Under a 15 A–30 A string current, this localized resistance generates intense Joule heat (P = I²R) that triggers thermal runaway.Because heat and oxidation reinforce each other, an overheating PV joint never self-heals. If you observe melted housing, charring, or thermal hotspots exceeding 10 °C–15 °C (ΔT) above adjacent cables, isolate the DC string before inspection and never disconnect a solar connector under load.
What made the connection overheat matters more than which connector gets replaced. Damaged plastic is evidence of heat, and the heat has a source somewhere in the installation. Leave the assembly, compatibility or cable-management problem in place, and a new connector pair will fail the same way at the same position.
Key takeaways
- Field termination errors and cross-mating dominate failures: Over 70% of melted solar connectors trace back to non-calibrated field crimps or mating incompatible “MC4-compatible” brands together.
- Verify with three quantitative checks: Combine IR thermography (checking ΔT against the cable), four-wire contact resistance testing (verifying ≤ 0.5 mΩ per IEC 62852), and mechanical pull-force testing before re-commissioning.
- Always replace both halves as a matched pair: Once thermal deformation or charring reaches the PPO/PA housing or tin-plated copper contacts, cut back the heat-damaged cable and install a certified matched pair—never clean and reuse a heat-stressed connector.
Safety note: PV DC circuits remain energized in daylight, and most PV connectors are not load-break devices. Do not disconnect, open, probe or repair a connector under load. Inspection and corrective work belong to qualified personnel, working to the connector manufacturer’s instructions and the electrical code adopted at the site.
| Possible cause | Typical clues | How a qualified technician verifies it | Corrective direction |
|---|---|---|---|
| Improper crimp or terminal assembly | Heating at the cable entry; discolored terminal; loose or damaged strands | Checks conductor size, strip length, terminal position, crimp geometry and assembly against the manufacturer’s instructions | Remake the termination with the specified cable, terminal, die and tool |
| Cross-mated brands or models | Different markings on the two halves; hot mating interface | Identifies both part numbers and checks documented intermatability or listing | Replace with an approved, documented mating combination |
| Incomplete mating | Locking tabs not fully engaged; visible gap; heating at the interface | Checks engagement using the manufacturer’s prescribed method | De-energize, replace damaged parts, and remate per instructions |
| Moisture, dirt or corrosion | Corrosion, residue, cracked housing, damaged seal, or a history of uncapped connectors | Inspects the sealing system, cable fit, housing and contacts after safe isolation | Replace affected components and correct the sealing or installation problem |
| Wrong cable, connector or current application | Heating at the termination; wrong cable diameter or conductor cross-section; overloaded branch | Compares part numbers, conductor size, cable diameter, current, ambient temperature and derating data | Select a cable-and-connector system with adequate ratings |
| Disconnection under load | Arc marks, pitting, soot or damage found after maintenance | Reviews maintenance history; examines contact surfaces after safe isolation | Replace arc-damaged parts and correct the isolation procedure |
| Mechanical stress or poor cable management | Connector hanging by the cable; sharp bend at the gland; movement or crushed housing | Inspects support, bend radius, strain relief, routing and movement | Replace damaged parts and secure the connector without loading the interface |
| Damaged, aged, counterfeit or nonconforming parts | Cracks, deformation, missing or inconsistent certification marks, uncertain origin | Confirms traceability, certification, part numbers and condition | Use traceable, certified components from an authorized source |
Most solar connector overheating arguments at site level are about quantitative thresholds, not physics. Under international testing standards and field commissioning protocols, three benchmark measurements separate a healthy PV joint from a failing one:
Compare the connector housing with the solar cable it terminates under identical irradiance and load. A healthy joint typically runs within 2 K to 5 K (2 °C–5 °C) of its adjacent conductor.
Under IEC 62852:2014+A1:2020 type testing, maximum temperature rise at rated current must not exceed 45 K (45 °C), and total operating temperature must stay within the housing’s upper limiting temperature (typically 105 °C to 115 °C).
Measure across the mated pair using a four-wire micro-ohmmeter and compare it with the datasheet value at ambient temperature.
Per TÜV Rheinland’s IEC 62852 test routines, initial contact resistance must remain ≤ 0.5 mΩ (and must not exceed 150% of its initial value or 0.75 mΩ after thermal cycling and damp-heat aging).
High-grade connectors like the PVLinkTech MC4/PV4 solar connector are engineered for < 0.35 mΩ initial contact resistance.
A connector system is qualified as a matched conductor, terminal, and crimping tool combination.
Under IEC 62852 / IEC 60352-2 mechanical pull-out testing, a properly crimped solar termination must withstand at least 310 N for 4 mm² (12 AWG) PV wire and 360 N for 6 mm² (10 AWG) PV wire without conductor slippage.
Always verify the applicable wire size, terminal specification, crimping tool and test procedure before using a pull-force result to accept or reject a termination.
Two standards frame those numbers. IEC 62852:2014+A1:2020 covers PV DC connectors up to 1500 V DC and 125 A per contact. It classes them as connectors without breaking capacity that may still be engaged and disengaged under voltage. In the United States, NEC 690.33(C) requires both halves of a mating pair to be the same type and brand, or listed as intermatable.
Treat every threshold as model-specific. Usable current depends on conductor size, cable construction, ambient temperature and the derating published for that exact part number.
Solar connector overheating begins with resistance. Every conductive joint has some, and current through it dissipates power as heat according to:
The behavior is not linear in practice. As the joint warms, its resistance increases, which produces more heat. A modest contact problem can move from warm to damaged faster than the string current suggests, because current barely changes while the joint fails.
Contact resistance has two parts. Bulk resistance is the material itself. Constriction resistance is current squeezing through the small areas where two metal surfaces actually touch. Crimp pressure, contact spring force and surface condition set how large those areas are. That is why a loose joint and a corroded joint can behave the same way electrically.
Overcurrent protection is sized for the circuit, not for one joint. A string at its normal current can carry a joint dissipating tens of watts in a spot a few millimeters across. The breaker sees nothing unusual. That case, and what failure marks on a housing tell you, is covered in our breakdown of a melted MC4 connector that kept the system running .
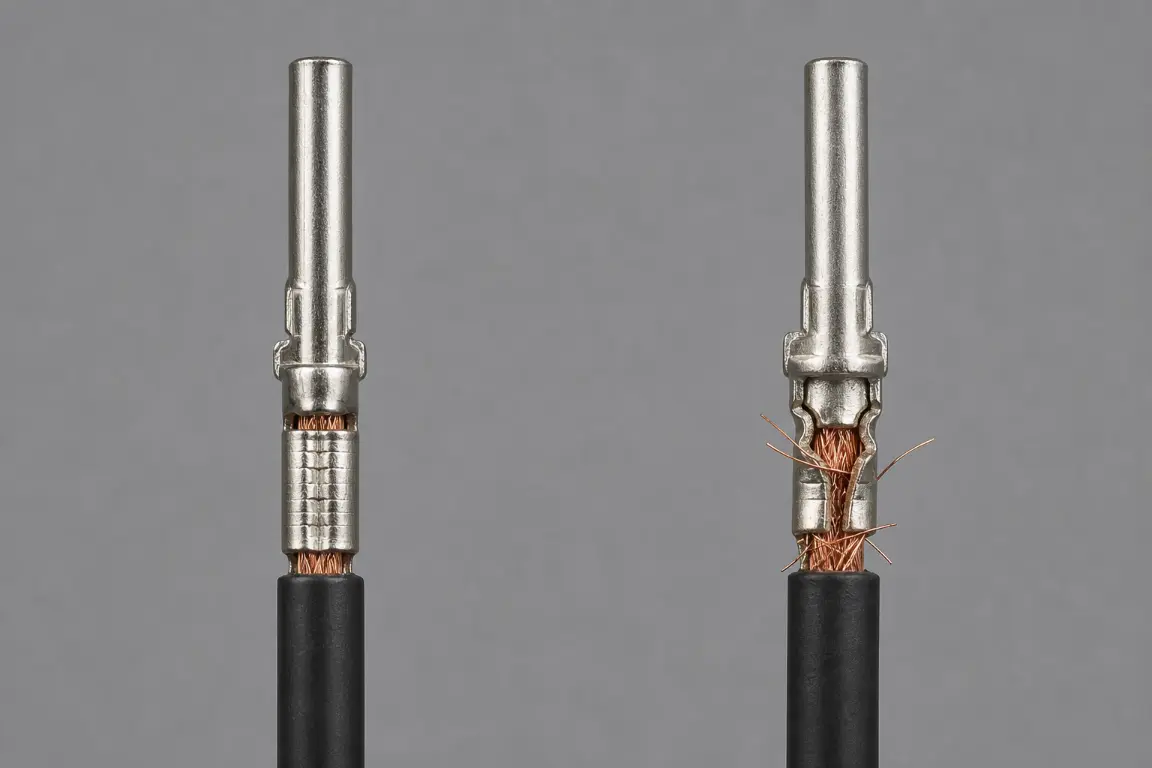
The cable-to-terminal crimp is the most heavily loaded interface in a PV connector. The conductor is not inserted to the required depth. The strip length is wrong. Strands are cut or missing. The terminal does not match the conductor size. An unapproved tool or die closes the barrel.
Every one of those defects cuts the metal-to-metal contact area, and less contact area means more resistance at the same current. The damage then compounds: thermal cycling works the strands loose, movement opens the joint slightly, and resistance creeps up over the string’s life. In field investigations the crimp is usually the one interface never checked against the connector’s own assembly specification.
Prevention: Follow the assembly instructions for the exact part number. Use the specified cable, terminal, strip length, tool and die, then complete the manufacturer’s dimensional and engagement checks. Factory-assembled leads remove that field variability, but they still need correct integration. Our comparison of crimped and soldered terminals covers what each method does to the conductor; the crimping walkthrough covers tool, die and strip length.
| Item | Where the value comes from |
|---|---|
| Cable type, conductor class and outer diameter | Approved cable range in the connector datasheet |
| Conductor cross-section | Connector datasheet |
| Terminal or contact part number | Connector drawing |
| Crimp tool and die | The tool and die the connector system was qualified with |
| Strip length | Connector drawing |
| Engagement check | Manufacturer’s installation instructions |
| Pull test and resistance limits | Manufacturer’s specification, or the applicable test standard |
A strip length, die number or torque figure copied from another product is not evidence that the termination is correct. Where a supplier cannot state the tool and die the connector was qualified with, the assembly cannot be checked against its own specification, and that gap belongs in the procurement decision.
Two PV connectors can latch together and still be a poor electrical pair. Contact geometry, contact force, tolerance stack-up, sealing and materials differ between families. A pair that was never qualified together can develop a smaller contact area, a weaker seal, or both.
In the United States, NEC 690.33(C) requires connectors of different types or brands to be listed and identified for intermatability as described in the manufacturer’s instructions. Local requirements depend on the code edition the authority has adopted. Most cross-mating on site happens between two families that look alike and are both sold as “MC4 compatible”. That is a market phrase, not an electrical statement.
Prevention: Record the manufacturer and complete part number of both halves. Use one approved connector system unless a specific cross-brand combination is documented as intermatable. If one half is unknown, treat the pair as unmatched. Our MC4 and PV4 connector differences note is the quick check, and approved halves are listed on the PV4-style solar connector page.
A connector that is not fully engaged can look connected while the locking mechanism is not seated. The contact area at the pin-and-socket interface is then smaller than designed, and less stable under load. Movement wears the plating, fretting corrosion follows, and resistance climbs from there.
The causes are mundane: a latch that never clicked, contamination in the coupling, an installation made in poor light with gloves on, or a locking feature already damaged by an earlier event. The failure is silent at first, and it shows up later as one hot connector at the end of a string.
Prevention: Mate exactly as the product instructions describe, and perform the prescribed engagement check instead of judging by feel. Do not force together parts that do not mate normally. Where a connector has already overheated, arced, deformed or lost locking integrity, replace the affected components. Do not push the halves back together and return the string to service.
An IP rating applies only when the correct components are assembled, mated and used with a compatible cable. Water and contaminants enter through a damaged housing, a cable outside its specified diameter range, a compromised seal, poor assembly, or an unmated connector left exposed without its cap. Once moisture reaches the contact or the crimp, corrosion reduces the real contact area while the sealing system degrades at the same time.
Visible corrosion also warns about scope. A corroded joint has usually been running hot, and that heat may have damaged the terminal, the strands and the insulation inside the housing.
Prevention: Keep unmated connectors clean, dry and capped with approved sealing caps. Replace contaminated, corroded, cracked or heat-damaged components. Do not apply grease, cleaner or sealant unless the manufacturer approves it for that product. On coastal, agricultural or washdown sites, exposure belongs in the replacement decision too: the IP67 versus IP68 comparison shows what each rating covers when a joint is mated, and when it is not. On these sites, moisture and solar connector overheating tend to arrive together, because corrosion raises resistance while the seal degrades.
A connector’s usable current is not one universal number. It depends on the connector model, conductor cross-section, cable construction, ambient temperature, certification basis, installation conditions and the derating the manufacturer publishes. A generic “30 A MC4” assumption is not a design input.
Both cable characteristics matter, for different reasons. The conductor cross-section drives electrical and thermal performance. The outside diameter decides whether the gland seals and whether the strain relief grips. A package that satisfies one and not the other produces either a hot joint or a wet joint. System changes follow the same logic. Adding modules in series raises voltage. Paralleling strings raises current in shared conductors and branch connections.
Prevention: Confirm the connector part number, the compatible cable type and diameter, the conductor size, the maximum circuit current, the ambient limits and the published derating, not the headline rating. The datasheet and the crimp-tool specification settle most of it; both are in our connector datasheets and drawings section. If you are still comparing families, the solar connector selection guide sets out the trade-offs.
Most PV connectors carry a “Do Not Disconnect Under Load” marking. IEC 62852 describes this class of connector as having no breaking capacity while still being capable of engagement and disengagement under voltage. Separating a pair while current flows draws a DC arc. Unlike an AC arc, it does not self-extinguish at a current zero. It can pit and erode the contacts, deposit conductive residue, and damage the housing.
This fault is usually created during maintenance rather than at installation. It follows a string that was isolated by switching something off instead of by verifying zero current at the connector.
Prevention: Use the site’s approved isolation procedure and confirm that no load current is flowing before separating a connector that is not rated for it. Replace the components that show evidence of arcing or thermal damage.
The electrical contact should not support the cable. A connector left hanging, pulled sideways, bent sharply at the gland, crushed by a cable tie or moved repeatedly loads the seal, the crimp and the mating interface at once. Movement is worse than static load, because it works the joint open in small increments and the damage stays invisible until resistance rises.
Tracker installations, wind, thermal expansion and routine maintenance all move cables. On a tracker the connector sees cycles every day rather than once a season.
Prevention: Support and route cables so the connector is not under tension, torsion, bending load, impact or repeated movement. Follow the manufacturer’s bend-radius, support and strain-relief requirements. Keep connectors clear of standing water and abrasive surfaces.
UV exposure, high ambient temperature, chemicals, impact, animals and earlier overheating all weaken housings and seals. Counterfeit and untraceable products are a separate problem. They may not match the construction, materials, tolerances or certification behind the markings they imitate, and the marking is not evidence of anything.
Age alone does not set a replacement interval. A connector in its tenth year can be in better condition than one installed two years ago on a badly managed tracker. Condition, environment, installation quality and inspection findings decide the answer, not the calendar.
Prevention: Buy traceable components from authorized sources and keep product and installation records. During scheduled maintenance, look for cracks, discoloration, deformation, damaged latches, poor support, corrosion and inconsistent markings. Our quality control process describes the checks a connector goes through before shipping, which is the record you should be able to ask any supplier for.
Solar connector overheating rarely announces itself with a failure. It shows up first as small changes at one joint. A symptom tells you where to look; it does not tell you what failed. The table below pairs what you actually see with the causes that can produce it, and with the check that confirms which one it is. Read the middle column as a list of candidates, not as a diagnosis.
| Symptom | Possible causes (candidates, not a diagnosis) | What a qualified person verifies |
|---|---|---|
| Warm housing, nothing visible | Early resistance rise at the crimp or the interface; joint running close to its published limit | Temperature comparison against equivalent connections under similar load; contact resistance |
| Brown or discolored plastic near the cable entry | Heat concentrated at the termination | Crimp geometry, strip length, conductor condition and terminal match against the part-number specification |
| Melted, deformed or dripping housing | Sustained over-temperature, usually after a resistance fault that went unchecked, or an unstable interface | Full replacement scope; condition of the mating half, cable and nearby insulation; the original cause |
| Blackened or pitted contacts, soot, arc marks | Arcing from separation under load, or a contact that was never stable | Both halves for replacement; the isolation procedure that was used |
| Cracked housing, damaged seal, corrosion at the contact | Moisture ingress from a cable outside its diameter range, a compromised seal, or an uncapped connector | Sealing system and cable fit; whether the assembly has also been running hot |
| One connector hot at the end of a string, the rest normal | Local resistance at that position, not a system-wide fault | Comparison with equivalent connections, then resistance measurement and a pull test after isolation |
| Connector loose on the cable, or it rotates | Failed crimp, wrong conductor or terminal size, or a contact that has moved in the housing | Assembly against the part-number specification, then replacement |
| Unusual smell, no visible damage | Insulation or plastic degrading from heat | Isolate and inspect. Smell narrows where to look; it does not identify the fault |
Two symptoms can appear together on the same joint, and one cause can produce different symptoms on different sites. That is why the confirmation step matters more than the symptom list. A melted housing proves the joint ran hot. It does not prove the crimp caused it.
Detecting solar connector overheating early costs far less than replacing a failed string section. Review alarms, production data and maintenance history first. Then inspect visually for discoloration, deformation, cracks, corrosion, loose support and mismatched markings. Use non-contact thermal imaging under suitable operating conditions.
Continue with electrical testing and disconnection only after an approved shutdown and isolation. Do not use a bare-hand touch test to judge whether a connector is safe, and do not disconnect a PV connector simply to find out whether it is hot.
If the cause is still not obvious after the visual check, the field sequence (pull test, resistance measurement, thermography) is set out step by step in our MC4 failure diagnosis checklist .
Infrared thermography shows a temperature difference. It does not name a cause. A single reading without a comparison is meaningless, because current, shade, wind and mounting all change surface temperature. The useful method is to compare connectors carrying similar current under similar conditions. Confirm any suspect joint with a resistance or pull test once the string is isolated.
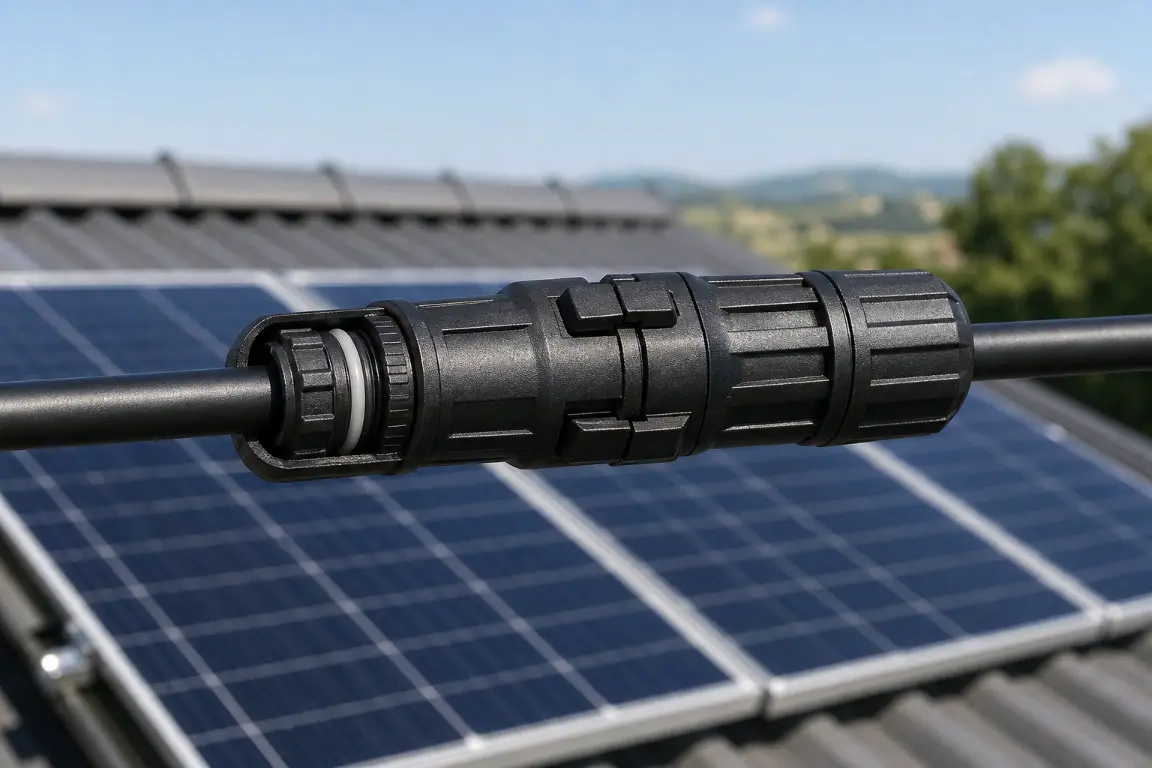
A connector that has melted, deformed, charred or discolored from heat cannot be cleaned back into service. It has already lost the properties that made it a connector: the housing geometry that holds the contact in position, the spring force behind the contact, and the seal that keeps water out were all exposed to the same heat that discolored the plastic.
Cleaning the outside does not remove what solar connector overheating leaves in the material, and a repaired-looking connector gives the next technician a false reading.
Replace the affected parts rather than returning them to service when you find any of the following:
The repair includes the mating half even when it looks intact, and it includes the cause: if the original crimp was made with the wrong tool, or the two halves were never qualified together, or the cable hangs from the connector, a new pair fails in the same position.
Repair scope, replacement parts and method belong to a qualified person working to the connector manufacturer’s instructions and the code adopted at the site. Use traceable parts from an authorized source, and record the connector part numbers on both halves, the cable size and what the inspection found. That record is what turns the next inspection from a guess into a comparison.
Standards, independent research and product specifications relevant to solar PV connector reliability, overheating assessment and field inspection.
Connectors for DC-application in photovoltaic systems – Safety requirements and tests. Refer to the official publication for the applicable scope, ratings and test requirements.
A connector testing reference covering relevant inspection and verification procedures. Consult the document for the specific contact resistance, temperature-rise and aging test methods and acceptance criteria it describes.
Research resources on PV connector reliability, cross-mating risks, thermal degradation and inspection considerations for photovoltaic systems.
Technical reference material on degradation and failure mechanisms in photovoltaic systems, including relevant issues involving junction boxes, cabling and DC connectors.
Product-level information for solar PV connectors and application-specific connector solutions. Verify the applicable model datasheet for rated current, voltage, ingress protection and supported conductor sizes.
Technical inquiry
If you are diagnosing solar connector overheating on a live string, our engineers can review the failure with you before you order. Send the connector part numbers on both halves, the cable type and conductor size, the system voltage and current, and what the inspection found, and we will confirm a compatible, traceable replacement set for that application.
Start a technical inquiry Email [email protected]
LET’S BUILD YOUR CONNECTION SOLUTION
Share your application, specifications, and estimated quantity. Our team will recommend a suitable connector solution and provide a quotation.
Low MOQ · OEM & ODM · Product Selection Support · Fast Quote Response